Tipping and swaging
BAS 100
- Tooth pitch
- 18 - 76 mm
- Tooth height
- from 10 mm
- Clearance angle
- 5 - 28°
- Front rake angle
- 5° - 35°
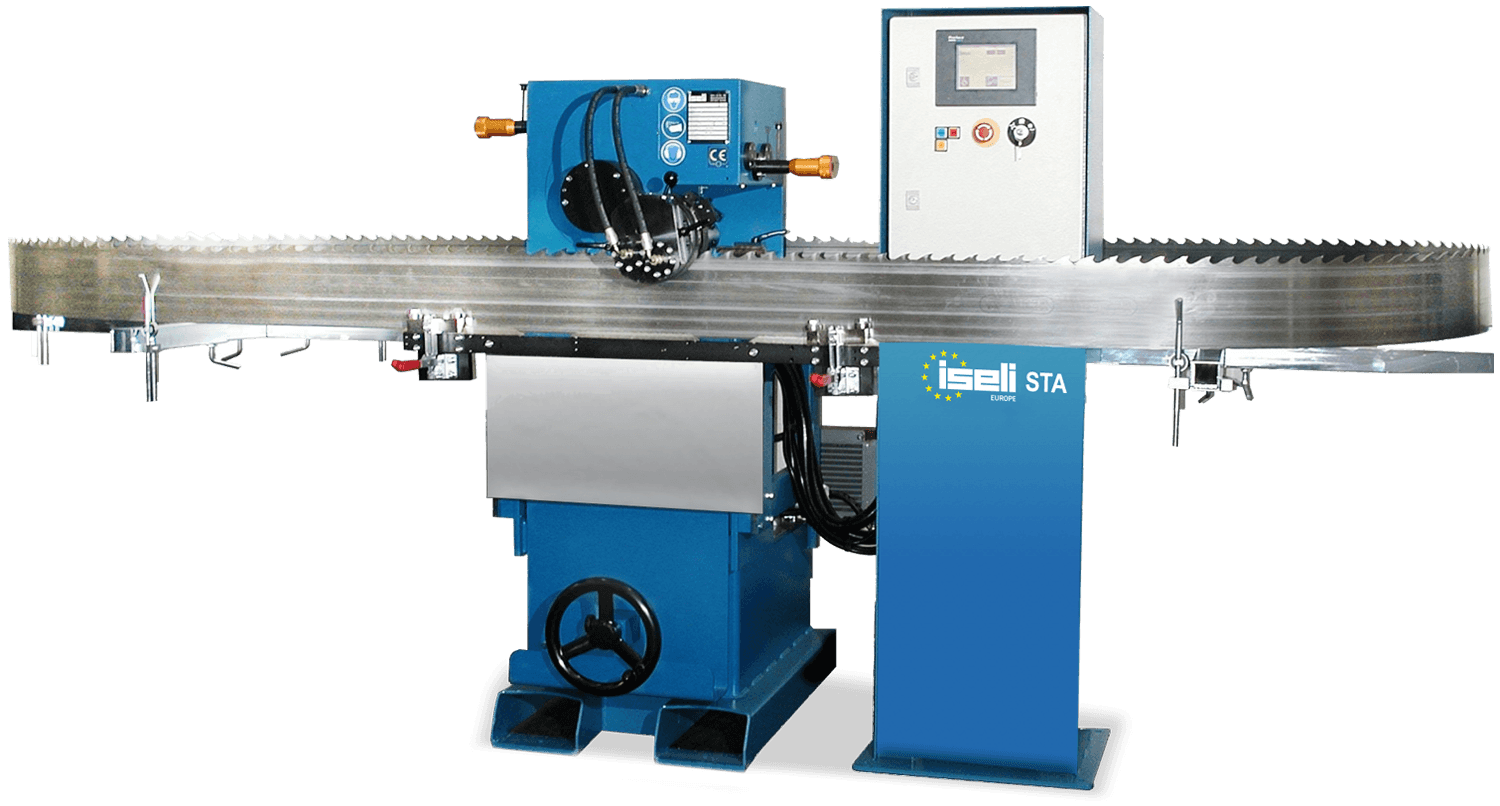
Description
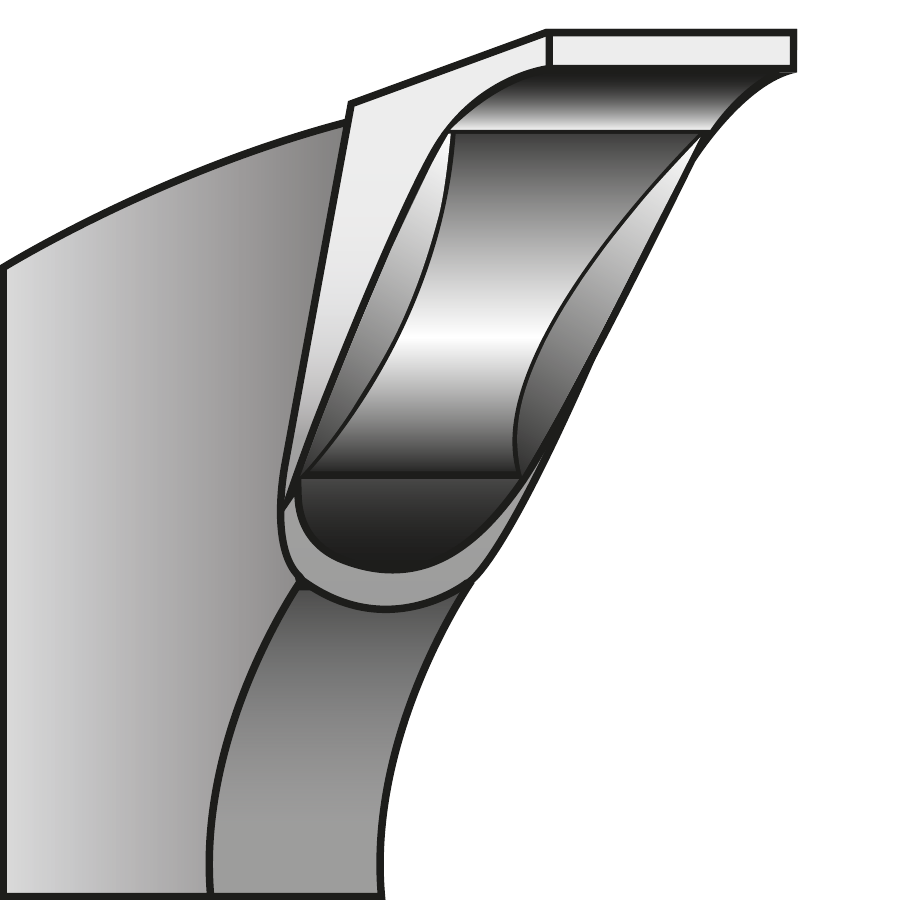
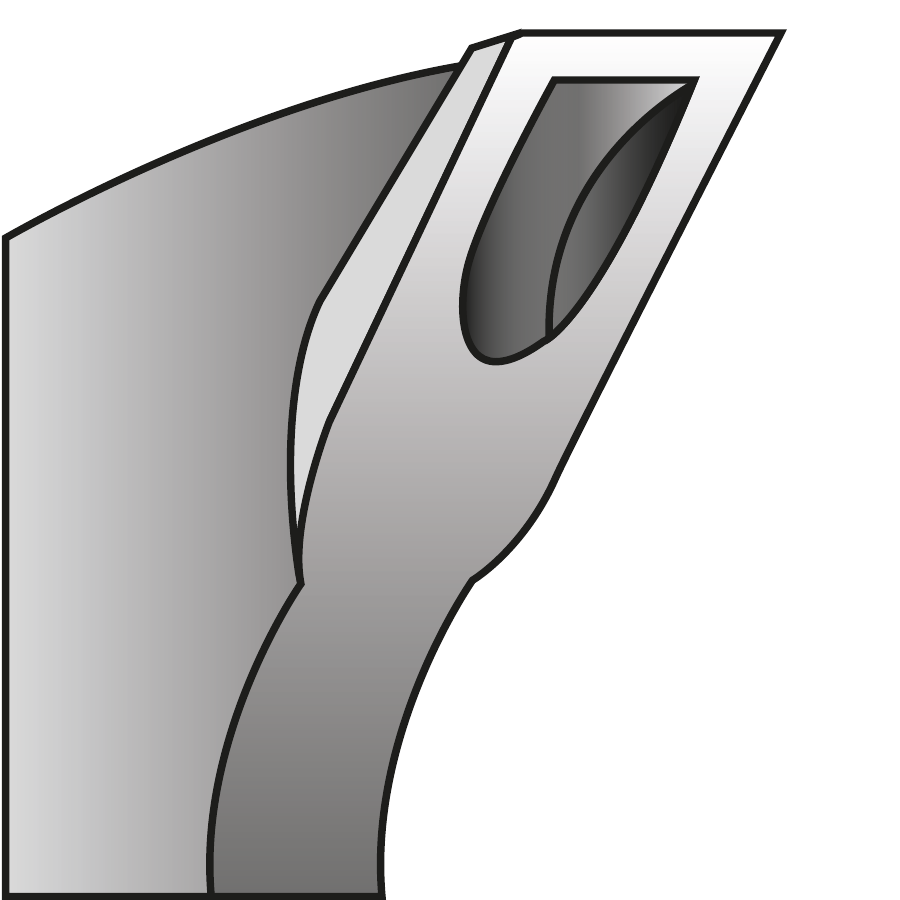
Swaging the saw teeth, in addition to setting, is another method to ensure that the saw remains free-cutting during operation. During the swaging process, a swaging eccentric is positioned in front of the saw tooth, which is held in place by an anvil. By rotating the eccentric, the saw material is displaced toward the tooth tip. Once the swaging process is complete, the eccentric returns to its original position.
Highlights
- The ISELI STA has a robust steel design. The machine is hydraulically controlled and equipped for band saws.
- The same tooth can be swaged once or twice and shaped in a single pass
- All the work processes are hydraulically controlled
- The blade feed is effected by the swage die so that accurate positioning of the saw tooth is guaranteed
- Swaging densifies the tooth point of the saw tooth of what results in a smoother and more accurate cut of the wood and a higher production
- By swaging, the tooth tip of the saw tooth is compressed, thus achieving a longer working life
- The swaging excenter is mounted on both sides and can be moved axially. It can be used in 10 different positions
- The clearance- and the rake angle, the width to be shaped and the tooth pitch are easily set according to scales, without changing any machinery parts
Applications
Other stellite tipping and swaging machines
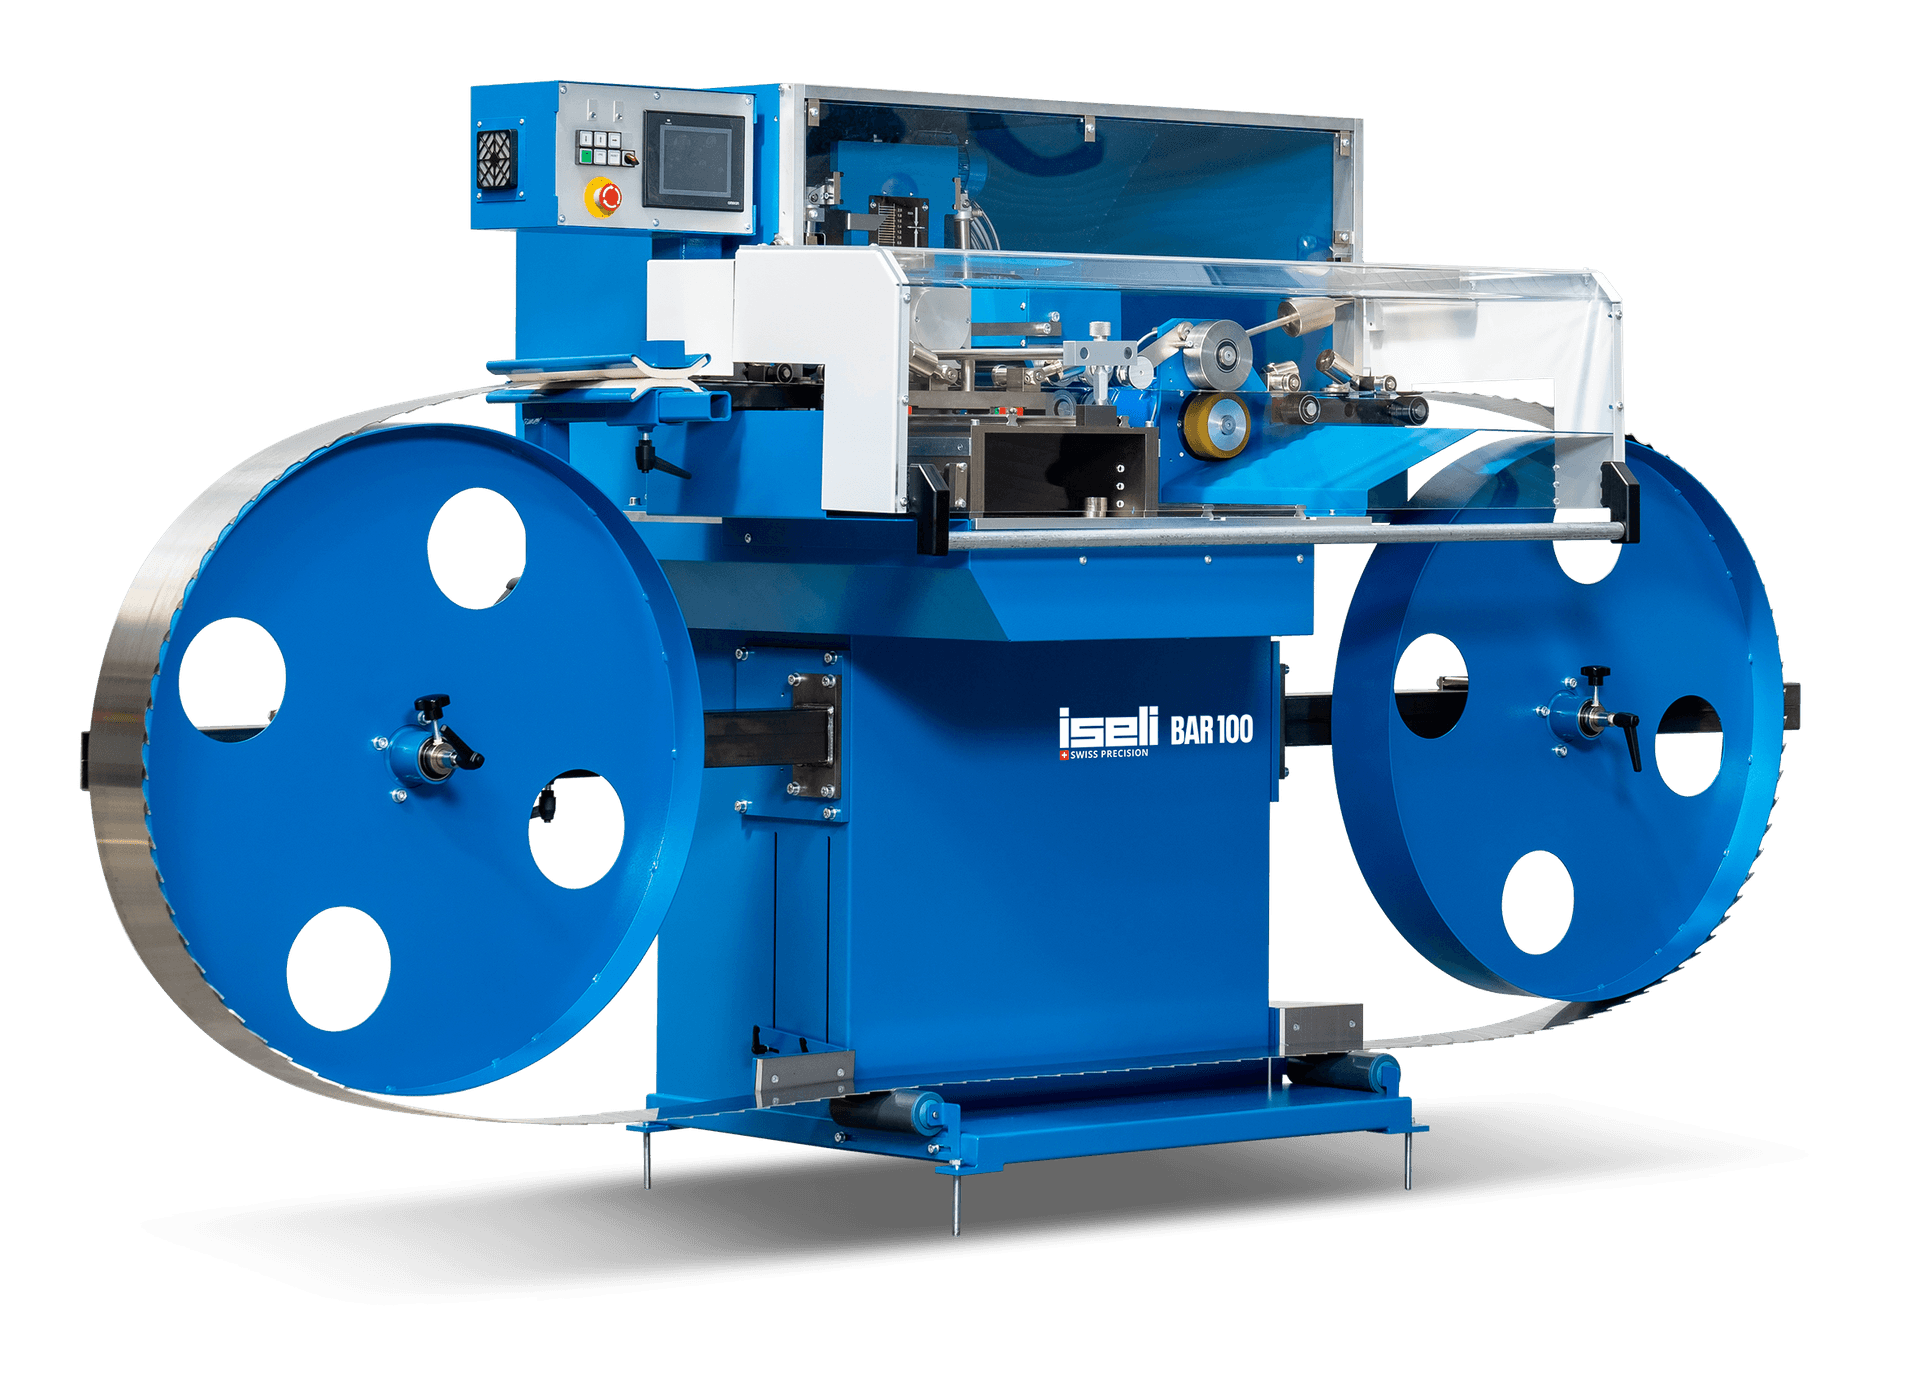 BAR 100Fully automatic levelling machine for band saw blades
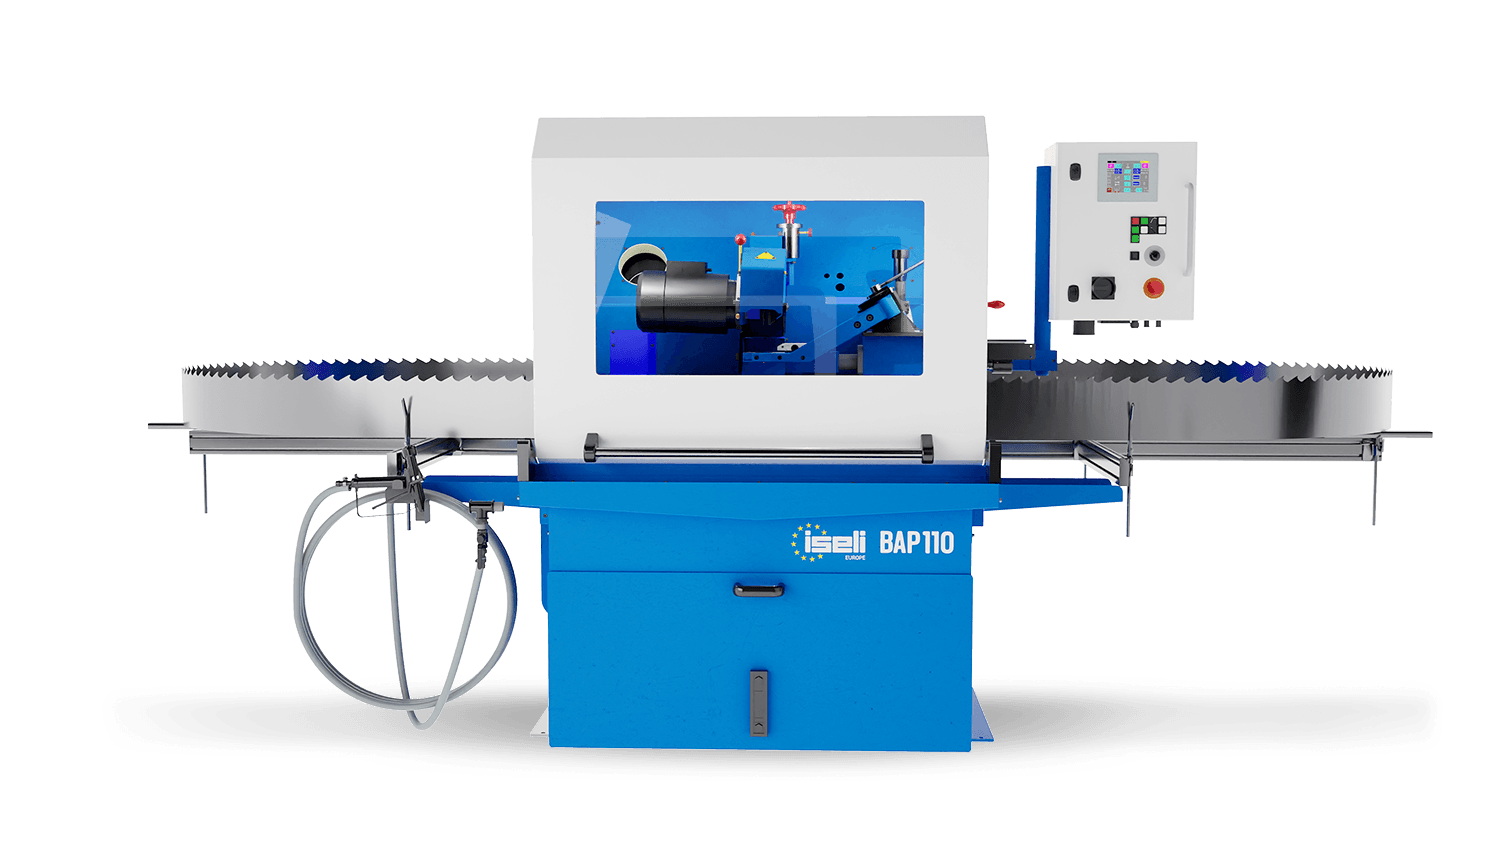 BAP 110Automatic profile sharpening machine for band saw blades
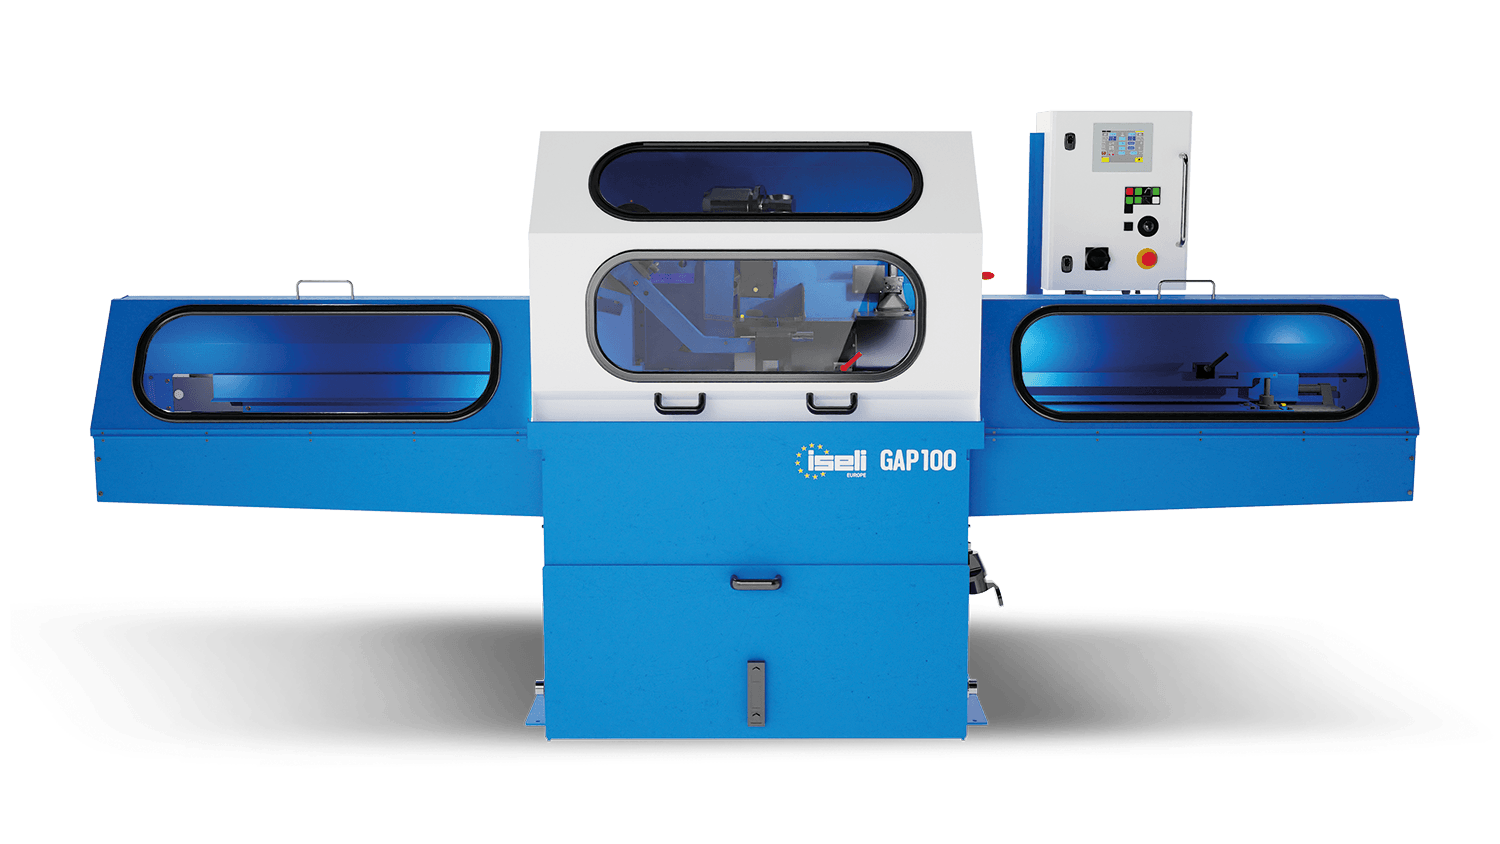 GAP 100Profile grinding machine for gullet saws, automatically mechanically cam-controlled
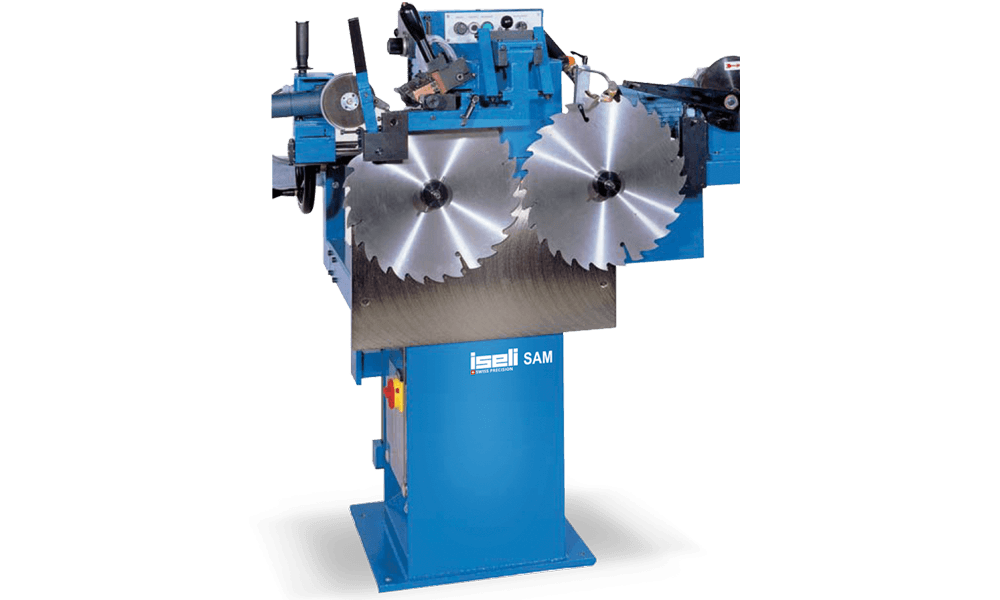 BMA 100Stellite welding machine for band, frame, and circular saw blades
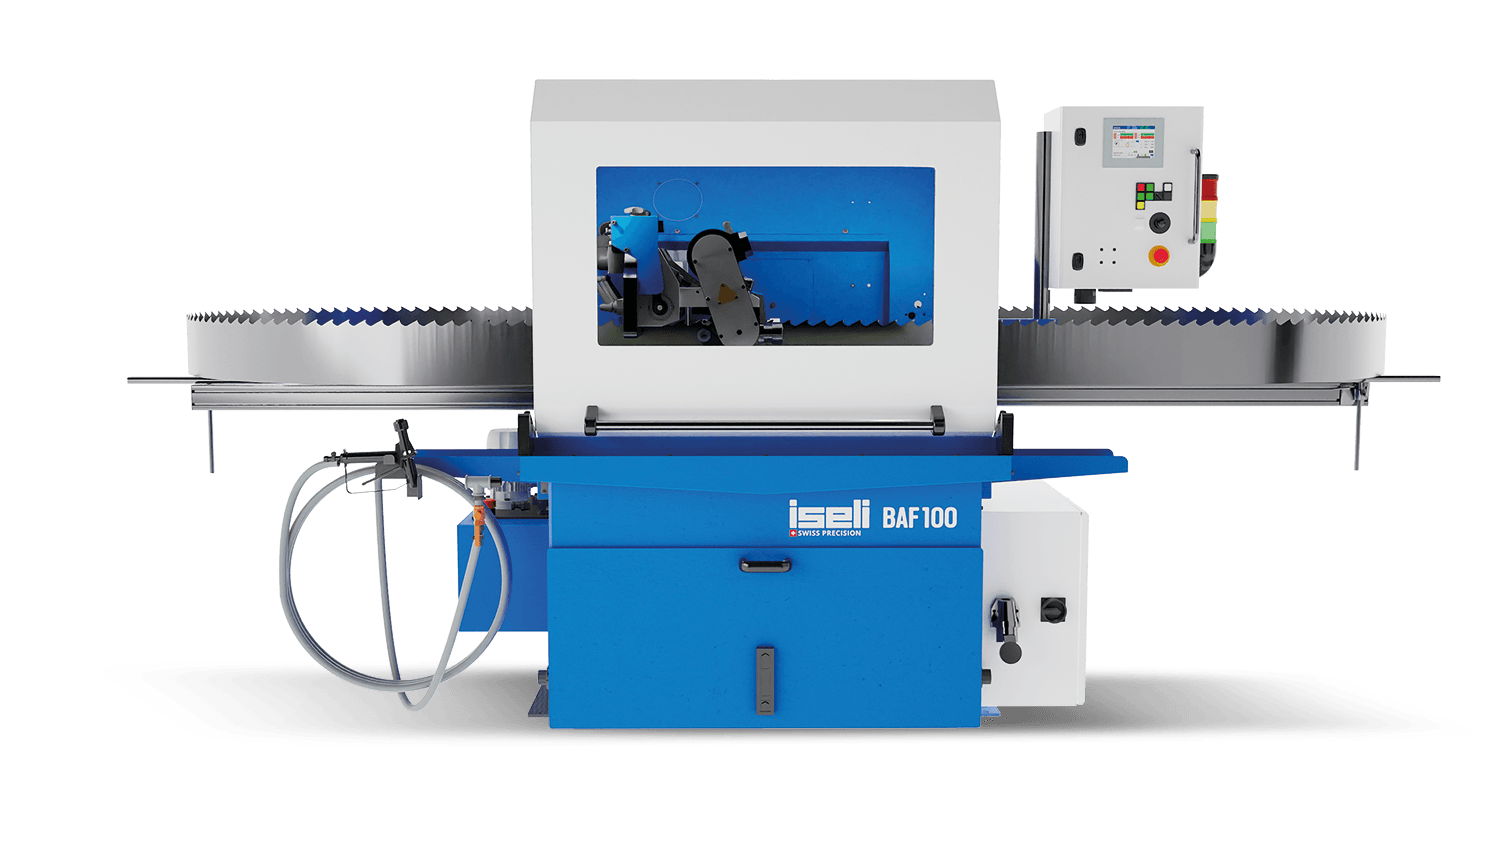 BAF 100Hydraulically controlled machine for automatic side grinding of band, circular and gang saws in wet grinding execution